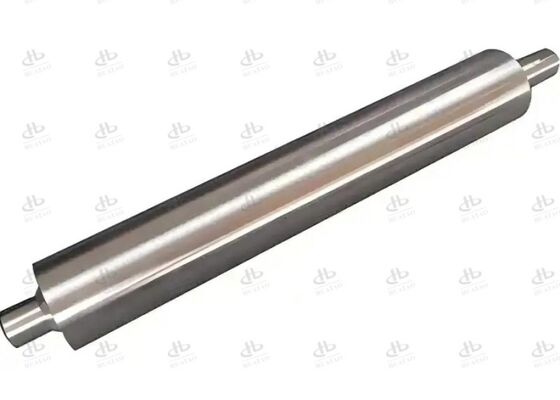
Oil-Heated Roller vs Electric Heating Roller: Which Is More Energy-Efficient for Film Production?
Quick Answer
A resistance-type electric heating roller converts 75–85% of its electrical input into shell heat, while a complete thermal-oil roller system delivers 65–75% after pump, piping, and rotary-joint losses — so on pure energy, electric wins. But the oil-heated roller holds a far flatter surface temperature (±1–2 °C with spiral channels vs ±5–12 °C for cartridges), which reduces scrap on BOPP/BOPET lines. Induction heating rolls outperform both: 90%+ efficiency, ±1 °C, no consumables, and roughly one-third of the energy per operating hour. The buying decision should be made on lifecycle cost per kilogram of saleable film.
Key Takeaways
· Electric beats oil on conversion efficiency; oil beats electric on temperature uniformity and thermal stability.
· Induction is the new benchmark: highest efficiency, tightest uniformity, lowest maintenance.
· Compare suppliers under identical loaded conditions, including TCU and pump power for oil systems.
· Oil-system energy consumption rises 15–20% in summer — always benchmark worst-season data.
· Above 200 °C, oil coking and element aging make induction the rational long-term choice.
Summary Table
| Item |
Thermal-Oil Roller |
Electric Cartridge Roller |
Induction Heating Roll |
| Function |
Heat film web via circulating oil |
Heat film web via internal elements |
Heat shell directly via eddy currents |
| Thermal efficiency (system) |
65–75% |
75–85% |
90–97% |
| Surface uniformity |
±1–2 °C (spiral) to ±10–15 °C (basic) |
±5–12 °C |
±0.5–1 °C |
| Max practical temperature |
~300 °C |
~320 °C |
400 °C+ |
| Service life |
2–3 years between overhauls |
1–2 years (element-dependent) |
10–15 years |
| Maintenance |
Oil changes, seals, flushing |
Element replacement 6–12 months |
Electrical inspection only |
Knowledge Graph: Where the Heating Roller Sits
Previous process: extrusion die → **CASTING ROLL** → cast sheet
Current process: heating roller (preheating) → temperature conditioning before orientation
Next process: **MDO STRETCHING ROLL** → MD stretching → TD oven → **PRS COOLING ROLL** → winding
The preheating roller on a **BI-ORIENTED FILM ROLLS** line is a 24/7 thermal load. Choosing its heating method is a multi-year energy commitment, which is why a structured comparison matters.
Working Principle of Each Heating Method
Thermal oil: a TCU heats synthetic oil to setpoint; a pump circulates it through internal channels. Channel design decides uniformity: straight bore (5–10 °C gradient), multi-pass U-turn (2–4 °C), or spiral helical flow (±1 °C class). The oil mass also acts as a thermal flywheel that absorbs load disturbances.
Electric cartridge: resistance elements in drilled bores conduct heat through the shell. Simple and cheap, but the stationary elements create periodic surface patterns; a failed cartridge makes a hard cold spot, and on/off cycling produces a sawtooth temperature curve.
Induction: static coils inside the roll generate eddy currents in the rotating shell itself — no medium, no transmission loss, zoned power capability, and no consumables. See our full engineering comparison: **ELECTROMAGNETIC INDUCTION HEATING ROLLS: PRINCIPLE AND PERFORMANCE**.
Energy Efficiency: The Measured Numbers
Published field data on 180 °C preheating duty (8 h continuous) reports approximately 120 kWh for oil systems, 95 kWh for cartridge rolls, and 35 kWh for induction rolls — heat-up to 200 °C takes 30–50, 30–40, and 18–20 minutes respectively. Two caveats: oil-system figures must include TCU heater and pump power, and all systems worsen with ambient temperature (oil circuits by 15–20% in summer). Compare at the wall, under load, at your worst season.
Material and Surface Comparison
Shell base: 45# forged steel or 4140 alloy for oil and induction rolls; stainless 304/316 where corrosion matters. Working surface: hard chrome for most preheating duty, PTFE where release is critical (kept thin — PTFE insulates), ceramic for abrasive duty. Surface roughness Ra 0.01–0.4 μm keeps film release consistent; an over-rough face traps air and forces operators to raise setpoint, wasting energy.
Application Comparison by Operating Condition
| Condition |
Best-Fit Method |
Why |
| ≤120 °C auxiliary heating |
Water/oil |
Safe, cheap, stable |
| 120–200 °C BOPP/BOPET preheating |
Spiral-channel oil or induction |
Oil proven and cheaper; induction if scrap matters |
| Above 200 °C continuous |
Induction |
No coking, no element aging |
| ±1 °C uniformity (optical/separator) |
Induction or spiral oil |
Only these reach the class |
| Frequent start/stop, small batches |
Induction |
Fastest heat-up and recovery |
| Minimum capex retrofit |
Electric cartridge |
No TCU/piping needed |
Industry Application Matrix
Selection Guide (5 Questions to Your Supplier)
1. Required kW at my maximum throughput — calculated, not estimated?
2. Guaranteed cross-web uniformity under polymer load, with an infrared map?
3. Worst-season energy figure including all peripherals?
4. Written component life: oil interval, element interval, seal life?
5. Mechanical acceptance: runout ≤0.005 mm, cylindricity ≤0.01 mm, dynamic balance report?
Procurement Guide
Provide each bidder the same inputs: polymer and grade, max throughput (kg/h), sheet width/thickness, line speed, setpoint temperature, ambient and coolant extremes, available electrical power, and installation space for TCU/piping. Require an itemized quotation, material certificates, hydrostatic test of oil circuits, and a spare-parts list. HUATAO manufactures to drawing with full inspection reports — see **ABOUT US** and our **CASE STUDIES**, including a 7.4 m BOPP line that cut roller procurement costs by over 60%: **CHROME-PLATED CHILL ROLLS: SOUTH AMERICAN 7.4M BOPP CASE**.
Failure Analysis
| Problem |
Possible Cause |
Recommended Solution |
| Hot spots on shell |
Failed cartridge / coked oil channel |
Replace element; flush and descale circuit |
| End-to-center gradient >5 °C |
Straight bore / edge cooling |
Upgrade to spiral channels; end-zone compensation |
| Slow recovery after web contact |
Fouled circuit / undersized TCU |
Clean channels; verify pump flow and heater kW |
| Sawtooth temperature ripple |
PID cycling of elements |
Add thermal mass; tune PID; consider induction |
| Oil leakage at rotary joint |
Worn seals |
Scheduled seal replacement; leak detection |
| Cold stripe on film |
Single element failure |
Staggered element layout; predictive replacement |
| Gradual energy creep |
Scale/coking buildup |
Baseline flow/ΔT logging with deviation alarm |
Maintenance Guide
· Daily: check bearing temperature (<70 °C), listen for abnormal noise, verify setpoint stability.
· Weekly: inspect oil level/pressure (oil systems), scan face temperature at steady state.
· Monthly: test element insulation (electric), check rotary-joint seals, clean face.
· Quarterly: verify pump flow and ΔT against baseline; inspect piping insulation.
· Yearly: thermal-oil analysis and replacement; full runout and balance verification.
· Records: keep a temperature-map history — drift reveals internal fouling months before product defects do.
Case Study
Customer Type: BOPET film producer (East Asia). Film Type: 12 μm optical-grade BOPET. Operating Conditions: preheat 165 °C, 350 m/min, 24/7. Problem: cartridge-heated preheating roll showed ±9 °C cross-web variation; scrap 2.8% on optical grades; element replacement every 8 months with 2-day downtime each. Solution: replaced with an induction heating roll with zoned power modules and a full acceptance protocol (cross-web map under load, runout, balance report). Result: uniformity within ±1 °C, scrap below 0.5%, energy on the preheating section down by roughly 60%, payback achieved in under two years through scrap and downtime savings.
Contact
Jenny Liu
Email: sale05@huataogroup.com
Website: https://www.huataomulti-indusrolls.com/
Mobile: +86 17743789775 (WhatsApp / WeChat)
Hashtags
#OilHeatedRoller #ElectricHeatingRoller #InductionHeatingRoll #BOPP #BOPET #PreheatingRoller #EnergyEfficiency #ThermalOil #IndustrialRoller #FilmExtrusion #HUATAO #RollerManufacturer #B2B #Procurement #FilmIndustry #StretchingLine #TemperatureControl #MachineBuilding #PlasticFilm #FactoryDirect

 Your message must be between 20-3,000 characters!